Carbide earns its price in the parts nobody sees: the punch behind a stamped panel, the nozzle that holds a bead for a million cycles, the seal face that runs against abrasive slurry. The catalogue shapes are cheap and everywhere. The reason to talk to a shop is the non-standard one — where the geometry, the cobalt content and the edge preparation decide whether it lasts a month or five years.
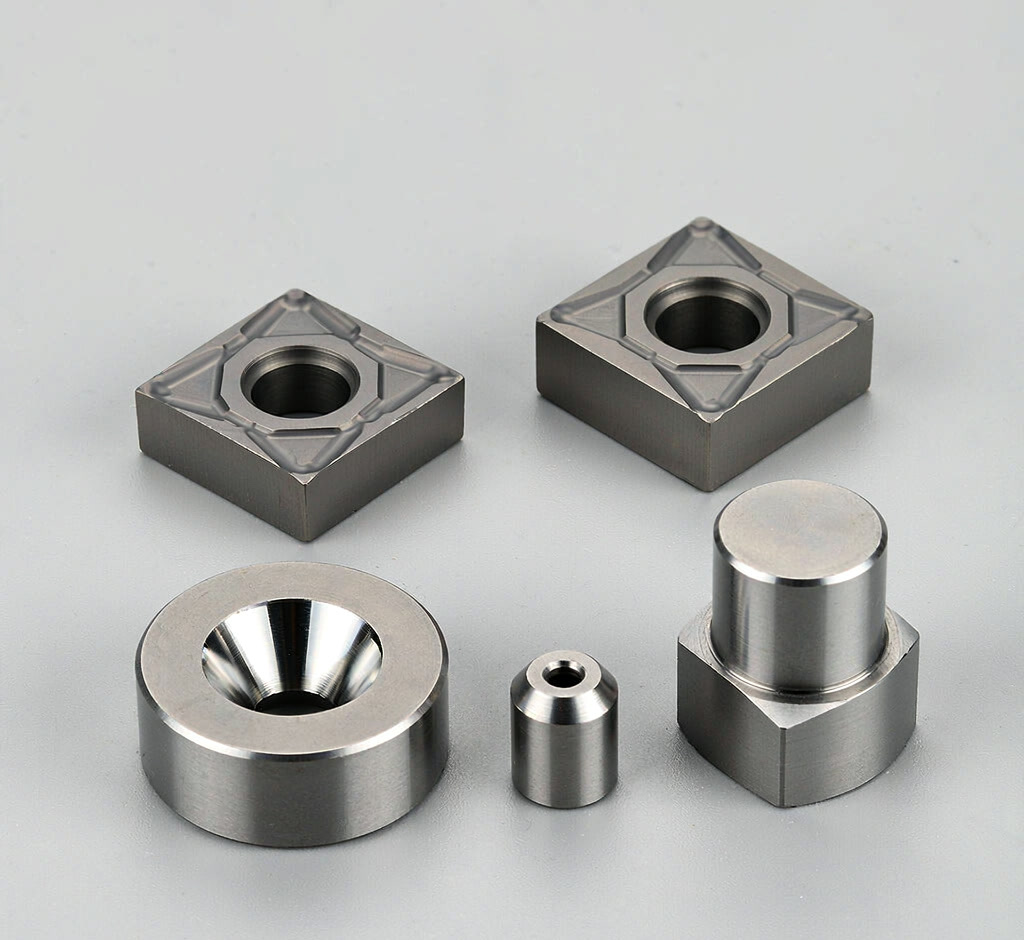
"Tungsten carbide" describes a family, not a material. The cobalt binder percentage decides the trade you are making, and two shops quoting "WC" at different cobalt levels are not quoting the same part.
| Cobalt | Hardness | Behaviour | Where it belongs |
|---|---|---|---|
| 6–8% | Highest | Wear-resistant, brittle under shock | Nozzles, seal faces, light finishing punches |
| 10–15% | Middle | The usual compromise | General punches, dies, form tools |
| 18–25% | Lower | Tough, deforms before it breaks | Impact work, coarse blanking, rolls |
| TiC-steel | Lower than WC | Machinable, weldable, cheaper | Large form tools where WC is impractical |
Ranges above are the standard trade-off in the WC-Co system, not a specification of the stock on our shelf. On the quote the grade is named with its cobalt figure, because "carbide" alone tells you nothing about which of these four you are buying.
Diamond grinding to size, wire and sinker EDM for profiles that cannot be ground, lapping on seal faces, edge preparation and chamfering. ±0.02 mm on ground features as the site standard, tighter on a named feature where the drawing asks.
Sintered blanks come from carbide plants; PVD and CVD coatings run at a coating shop. Both are named on the quote as their own line. This shop does not press powder and does not run a coating chamber.
Critical dimensions recorded per part, edge condition checked under magnification, and the reading log shipped with the batch. Hardness is the blank maker's certificate, not our claim.
Almost every carbide part that fails early fails for one of these reasons, and four of the five are decided before the part is cut.
Carbide does not deform, it breaks. A dead-sharp internal corner is a crack starter. Specify a 0.2–0.5 mm radius or a chamfer; if the drawing shows a sharp corner, we will ask before making it.
Water-based coolant, food contact or mild acids attack the cobalt binder and leave a porous surface that wears fast. Grade choice and passivation matter more than hardness here — tell us the medium, not just the load.
Wire or sinker EDM leaves a thin, brittle recast layer. On a sliding or sealing face it spalls and takes the tolerance with it. The fix is a ground or lapped finish after EDM, which is a separate line on the quote.
The hardest grade available is the wrong answer for anything that sees impact. If the part is a punch, tell us the material it hits and the stroke rate — that decides cobalt content more than a hardness number does.
A seal ring with a good Ra and a bad flat reading leaks. Flatness and parallelism belong on the drawing next to the roughness; without them, "lapped" means nothing checkable.
Carbide parts do not all fall under one tariff line. We put the description and the material on the commercial invoice; the tariff classification and the declaration are your forwarder's job, not ours to guess at.
Catalogue shapes are cheaper somewhere else. The reason to send this drawing to a shop is that the geometry is awkward, the batch is small, and someone has to say honestly whether it can be ground at all.
Send a drawing for review